


1. Recycled PVC Raw Material Pretreatment
Raw material quality determines the finished product performance. This step cannot be skipped for recycled PVC.
- Sorting: Remove foreign objects, other plastic contaminants and heavily aged PVC fragments.
- Crushing & grinding: Break waste PVC materials into uniform regrind particles.
- Washing & drying: Clean dust, mud and surface pollutants; fully dry particles to eliminate moisture.
- Inspection: Test heat stability and impurity content of recycled PVC batches before feeding.
2. Formula Mixing
Mix recycled PVC particles with functional additives in a high‑speed mixer.
Key additives:
✅ Heat stabilizer: Resist thermal decomposition during extrusion
✅ Lubricant: Improve material flow and prevent sticking to screw & die
✅ Filler: Adjust hardness and production cost
✅ Impact modifier: Enhance impact resistance for door‑window usage
Note: Compared with virgin PVC, recycled PVC usually requires extra stabilizer due to material aging.
3. Extrusion Plasticization
Prepared compound material is transported to the twin‑screw extruder.
- Feed zone: Stable and even feeding, avoid material bridging.
- Plasticizing zone: Control barrel temperature reasonably. Too high will trigger PVC decomposition; too low causes poor plasticization.
- Shear control: Adjust screw speed. Excessive shear will generate extra heat and damage recycled PVC molecular structure.
4. Forming & Vacuum Calibration
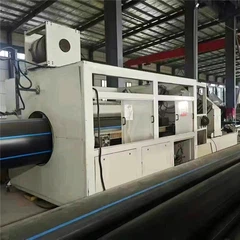
Melted PVC flows through the special door‑window profile die, then enters the vacuum calibration tank.
- Vacuum sizing keeps precise outer dimension and profile geometry.
- Gradual water cooling prevents quick temperature drop which may result in internal stress and later deformation.
5. Haul‑off, Cutting and Post‑Processing
- Haul‑off machine maintains constant pulling speed. Speed mismatch will lead to thickness deviation.
- Fixed‑length cutting according to order requirements.
- Optional post‑treatment: surface polishing, punching, chamfering for installation needs.
6. Quality Inspection and Packing
Finished profiles go through full checks: dimension measurement, surface appearance inspection, impact test. Defective products can be crushed and recycled again. Qualified goods will be bundled and packed for shipment.
Conclusion
Recycled PVC door and window profile production is not simply re‑melting waste plastics. Strict raw‑material pretreatment, optimized formula and stable extrusion parameters are essential to get high‑quality end products. Each batch of recycled materials has different properties, so on‑site process adjustment is always necessary.
Hot Tags: used profile machine equipment, China used profile machine equipment manufacturers, suppliers, profile extrusion machine used for stretch blowing, used profile extruder for crown molding, used profile extruder for lightweight profiles, profile extrusion machine used for heat resistant profiles, second hand profile extruder for fine profiles, used profile extruder for square profiles